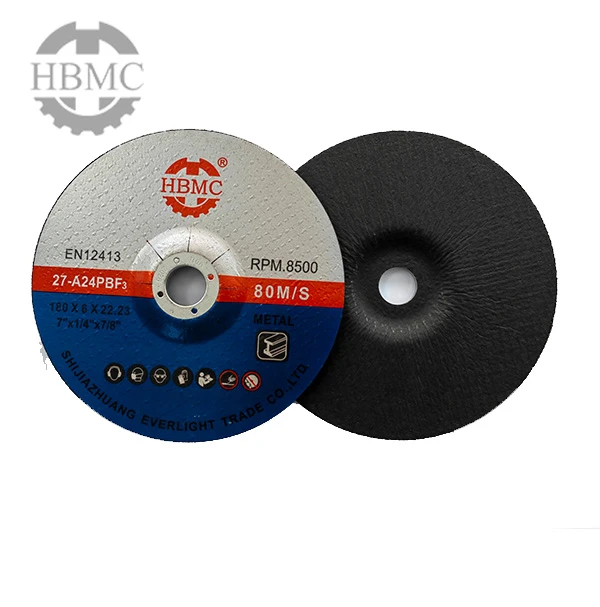
Cutting discs are high-frequency consumables widely used in metal processing, steel structure construction, mechanical polishing, pipeline processing, hardware forging and other scenarios. The wear rate of cutting discs is closely related to consumable procurement costs. Abnormal edge chipping and excessive wear will undermine operational stability. Improper operation techniques, equipment working conditions and storage methods adopted by many processing workers lead to premature failure and abnormal damage of cutting discs. Standardized operation, equipment commissioning, storage maintenance and other standardized measures can effectively extend the service cycle of cutting discs, reduce the frequency of consumable replacement and stabilize on-site processing rhythm.
1. Complete adaptive selection and appearance inspection before operation to avoid initial damage and scrapping
Most premature damage to cutting discs stems from hidden dangers formed before installation. When selecting cutting discs, users shall match the product with the thickness of cut materials, material hardness and equipment rotating speed. For high-hardness alloy steel and thick steel plates, cutting discs with matched hardness shall be selected; for thin plates and thin-walled pipes, thin cutting discs are applicable. Avoid using thick cutting discs to cut thin-walled workpieces, which will cause stress concentration on one side and edge breakage. Meanwhile, check the rated rotating speed of angle grinders and cutting machines, and ensure the maximum linear speed marked on the cutting disc matches the output rotating speed of the equipment. Operation exceeding the rated rotating speed will cause excessive structural stress of the cutting disc, resulting in cracking, fragmentation and direct scrapping.
Conduct visual inspection on newly unpacked cutting discs to check for cracks, gaps, moisture softening and edge collision damage on the disc surface. The binder strength of dampened cutting discs declines, and surface peeling is prone to occur during operation. Cutting discs with defects are prohibited from use. Keep the flange backing plate flat and clean, ensure the flanges on both sides are of the same size, and apply even and moderate clamping force. Excessive clamping force will cause internal stress cracking on the end face of the cutting disc due to extrusion. Reserve reasonable buffer space to ensure uniform stress during the rotation of the cutting disc.
2. Optimize cutting operation techniques to reduce eccentric wear and impact wear
Forcible pressing is the primary cause of rapid consumption of cutting discs. Keep the tool stable and perpendicular to the cutting seam during cutting operation, maintain linear feeding of the whole machine, and avoid large left-right swinging and tilting to pry the cutting disc. Inclined cutting will concentrate stress on a single edge of the cutting disc, triggering sharp edge wear, notch and block falling, rapidly reducing the effective cutting area and greatly shortening the overall service life.
Rely on the self-weight of the tool for uniform feeding during cutting, and avoid extra downward manual pressing. Forcible pressurization will lead to sharp rise of friction temperature of the cutting disc, rapid passivation and shedding of abrasive grains, failure of resin binder under high temperature, softening and deformation of the cutting disc, which not only reduces cutting efficiency but also accelerates overall wear. For cutting thick steel parts, adopt segmented cutting, gradually increase the single cutting depth and reserve heat dissipation gaps to avoid irreversible structural damage to the cutting disc caused by continuous heat accumulation during long-term uninterrupted cutting.
Clamp and fix workpieces firmly to prevent shaking and vibration during cutting. Vibration of workpieces will subject the cutting disc to alternating impact force continuously, leading to abnormal shedding of abrasive particles and uneven disc surface of the cutting disc. Unbalanced stress will be formed in subsequent cutting, creating a vicious cycle to accelerate wear.
3. Control continuous operation duration and implement intermittent heat dissipation and cooling
High-speed cutting generates massive friction heat. The high-temperature resistance of resin binder is limited. Continuous non-stop operation will lead to heat accumulation, decreased surface hardness and wear resistance of the cutting disc, reduced holding force for abrasive grains and large-area sand shedding. Set intermittent shutdown for heat dissipation during processing, suspend operation for natural cooling after completing a section of cutting work. Do not spray water directly on the high-temperature cutting disc, as sudden cold and heat will generate internal cracks inside the cutting disc, damage structural strength and bring hidden dangers of breakage.
Increase the frequency of intermittent heat dissipation appropriately when cutting high-temperature steel and heat-resistant alloys, adopt natural air cooling to lower the temperature, maintain the overall structural stability of the cutting disc and reduce irreversible aging wear caused by high temperature.
4. Standardize warehouse storage of cutting discs to prevent deterioration and failure during storage
The storage conditions of unused and temporarily replaced cutting discs directly affect their service conditions. Cutting discs shall be stored in a dry, ventilated and normal-temperature warehouse, away from rainwater, oil stains and corrosive liquids. Grease penetrating into the pores of the cutting disc will weaken the bonding effect, and dampened cutting discs suffer reduced toughness and are prone to breakage after installation.
Place flaky cutting discs vertically for storage, and avoid horizontal stacking under heavy pressure. Multi-layer stacking extrusion will cause bending deformation of the cutting disc and residual internal stress, which is easy to crack during high-speed rotation after installation. Store cutting discs of different specifications and types in separate areas to avoid edge collision damage during transportation. Check the status of long-term idle cutting discs regularly, and scrap those with dampness and deformation directly instead of putting them into production.
5. Maintain cutting host equipment regularly to ensure stable operating conditions
Equipment failures will indirectly aggravate cutting disc wear. Check the spindle clearance of the cutting machine regularly. Excessive spindle swing will cause large radial runout during high-speed rotation of the cutting disc, sharp increase of local friction and irregular wear. Replace worn bearings and aging shock-absorbing accessories in a timely manner to guarantee spindle concentricity.
Clean rust and metal burrs on the flange and rotating shaft. Foreign matters clamped between the flange and the cutting disc will cause uneven stress after clamping and eccentric wear during operation. Install the complete equipment protective cover. In addition to safety protection, the protective cover can block high-temperature iron scraps from continuous burning on the side of the cutting disc and reduce ineffective side wear.
6. Adopt proper tool retraction at the finishing stage to avoid instantaneous damage to the cutting disc during shutdown
Reduce feeding force and slow down the cutting speed when the workpiece is about to be cut off at the finishing stage. Reduce the stress on the cutting disc before the workpiece is completely disconnected. The impact force at the moment of workpiece fracture is likely to crack the edge of the cutting disc. Lift the cutting disc steadily away from the workpiece before shutting down the equipment after complete cutting. Do not shut down with load to prevent workpiece jamming from breaking the edge of the cutting disc.
Conclusion
Extending the service life of cutting discs focuses on implementing five key points: adaptive matching, stable operation, temperature control and heat dissipation, proper warehousing and equipment maintenance. Eliminate bad habits such as forced pressing, inclined cutting and swinging, overspeed operation and application of dampened cutting discs. These measures can effectively extend the service life of cutting discs, control the comprehensive cost of consumables, maintain flat cutting sections, reduce operational risks caused by cutting disc fragmentation, and adapt to various regular cutting operations such as steel structure processing, sheet metal fabrication, engineering construction and mechanical maintenance.