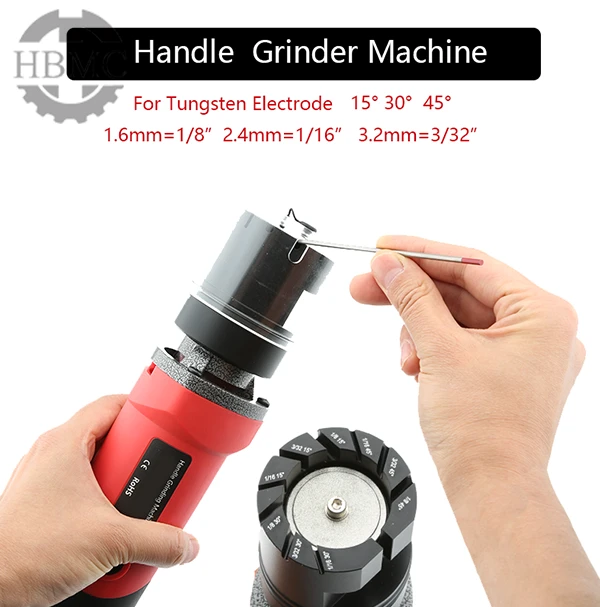
Tungsten electrode grinders are special-purpose equipment for standardized tungsten electrode preparation in TIG welding processes. They form regular tungsten electrode tips through grinding with abrasive wheels. Fine tungsten dust is continuously generated during grinding, which tends to adhere to the abrasive wheel, clamping chuck, grinding chamber and motor gaps. Implementing standardized daily cleaning and periodic maintenance can stabilize the grinding angle of tungsten electrodes, reduce tungsten inclusion welding defects, and prevent equipment jamming, motor overheating, premature failure and other faults. This document divides maintenance into end-of-shift daily cleaning and periodic deep maintenance, and also elaborates various problems arising from inadequate cleaning.
I. Basic Cleaning After Each Shift (Mandatory Daily Task)
Before carrying out any cleaning work, cut off the power supply of the equipment and wait until the abrasive wheel stops rotating completely to avoid safety hazards caused by accidental startup. Operators are recommended to wear dust masks and safety goggles during dust removal.
Clean the dust collection assembly
For models equipped with dust collection boxes or drawers, empty internal tungsten dust after every shift. For units connected to external dust extraction pipelines, clean the filter screens at pipeline connectors. Excessive dust accumulation will block airflow inside the chamber and cause dust backflow onto the abrasive wheel and fixtures. Collected tungsten dust shall be disposed of in accordance with solid waste regulations; sweeping dust onto the ground arbitrarily is prohibited.
Wipe the machine exterior and protective shield
Use dry brushes and lint-free cloths to remove dust from the transparent protective shield and machine housing. Keep the shield transparent for easy observation of grinding conditions. Do not flush the whole machine directly with water, as moisture entering the motor and electrical switches may cause short circuits. Stubborn stains on the housing can be wiped with a small amount of anhydrous ethanol; ensure full drying after wiping.
Clean the electrode clamping mechanism
Tungsten debris easily gets trapped in gaps of the chuck, collet and guide sleeve. Use a small brush to sweep dust from inside the jaws to prevent slipping caused by debris. Unstable clamping leads to eccentric grinding and inconsistent taper angles of tungsten electrodes, impairing arc stability.
Simple surface cleaning of the abrasive wheel
Sweep dust attached to the abrasive wheel surface with a soft brush. Once dust clogs the pores of the wheel, grinding resistance rises and may cause overheating and oxidation of tungsten electrode tips. Do not scrape the wheel vigorously with hard tools to avoid damaging the abrasive layer.
II. Periodic Deep Cleaning and Maintenance (Adjust frequency according to usage intensity)
Blow out the interior of the grinding chamber
After one week of continuous operation or high-volume grinding work, remove the protective shield and blow residual dust out of the chamber from outside to inside using low-pressure dry compressed air. Avoid excessively high air pressure, which may blow dust directly into motor bearings and gaps of electrical components. Focus blowing areas: surroundings of the abrasive wheel, chamber corners and electrode inlet/outlet passages.
Dressing and condition inspection of the abrasive wheel
When the wheel suffers surface clogging, partial wear or grooves, dress the working surface with a wheel dresser. Replace the wheel with a matching model promptly if edge chipping, extensive abrasive shedding or severe uneven wear occurs. Clogged wheels reduce grinding efficiency and tend to produce black oxide layers on tungsten electrode tips.
Disassembly and cleaning of the clamping chuck
Regularly disassemble the chuck and elastic collet to thoroughly remove tungsten dust trapped in gaps. Long-term dust buildup causes sluggish chuck opening/closing and reduced clamping force. After cleaning, inspect collets for deformation and wear; replace fittings in a timely manner if excessive clearance exists. Avoid contaminating clamping contact surfaces with oil during reassembly to prevent slipping.
Inspection and maintenance of transmission and moving parts
Check for abnormal noise or wobbling during spindle rotation; verify whether all fixing screws and shield fasteners are loose. Replenish grease to bearings periodically as specified in the equipment manual. Dust intrusion into bearings accelerates wear and causes operational vibration.
Dustproof inspection of electrical components
Clear dust from equipment cooling vents to guarantee motor heat dissipation; inspect power cable sheaths for abrasion. Accumulation of conductive tungsten dust on circuit boards and wiring positions poses a short-circuit risk.
III. Maintenance Guidelines for Long-Term Shutdown
Complete a full deep cleaning before long-term equipment deactivation and remove all dust. Leave the chuck slightly loosened to prevent permanent deformation of elastic collets under sustained compression. Store the machine in a dry, dustproof area covered with a dust cover, away from humid environments and welding spatter. Before restarting, conduct a no-load trial run and confirm no abnormal noise or vibration before putting it back into service.
IV. Common Problems Caused by Inadequate Cleaning and Maintenance
Reduced grinding accuracy and increased welding defects
Dust trapped inside collets loosens tungsten electrode clamping and causes offset during grinding, resulting in inconsistent taper angles. Tungsten dust blocking wheel pores increases grinding resistance, triggering overheating and oxidation of electrode tips. This frequently leads to tungsten inclusions, arc wandering and difficult arc initiation during welding.
Mechanical jamming and shortened service life of wearing parts
Fine tungsten dust continuously invades chucks, bearings and guide rails, acting as abrasive media and aggravating metal wear. Severe scale buildup on chucks hinders opening and closing and may even prevent electrode locking.
Motor overheating and shortened overall service life
Dust blocks heat dissipation channels, trapping heat generated during motor operation. Prolonged high temperatures accelerate coil aging. Dust entering the motor may cause short circuits and shutdowns in severe cases.
Workshop dust pollution and health risks
If dust collection boxes remain uncleaned, dust escapes outward during grinding, raising operators’ risk of inhaling fine tungsten dust and violating workplace occupational health requirements.
V. Warnings on Prohibited Practices for Cleaning and Maintenance
Do not flush the entire grinder directly with water; do not use oil-based cleaners inside the chamber, as oil mixed with tungsten dust forms hard-to-remove sludge; do not blow high-pressure air directly into the motor interior; do not disassemble protective shields or clean the abrasive wheel while the equipment is powered on. When alternately grinding tungsten electrodes of different materials, an additional chamber cleaning is recommended to avoid cross-contamination of electrode tips by foreign metal debris.
Summary
Cleaning and maintenance of tungsten electrode grinders consist of simple end-of-shift sweeping and periodic deep servicing. Key cleaning targets include dust collection units, protective shields, clamping chucks, abrasive wheels, grinding chambers and heat dissipation channels. Persistent neglect of cleaning work not only destabilizes tungsten electrode grinding quality and induces various welding defects, but also accelerates wear of bearings, motors and chucks, raising maintenance costs. Establishing standardized cleaning cycles and properly managing dust collection and component inspection can sustain tungsten electrode preparation precision and extend equipment service life.